Assembled, tested and signed off. Before it ships.
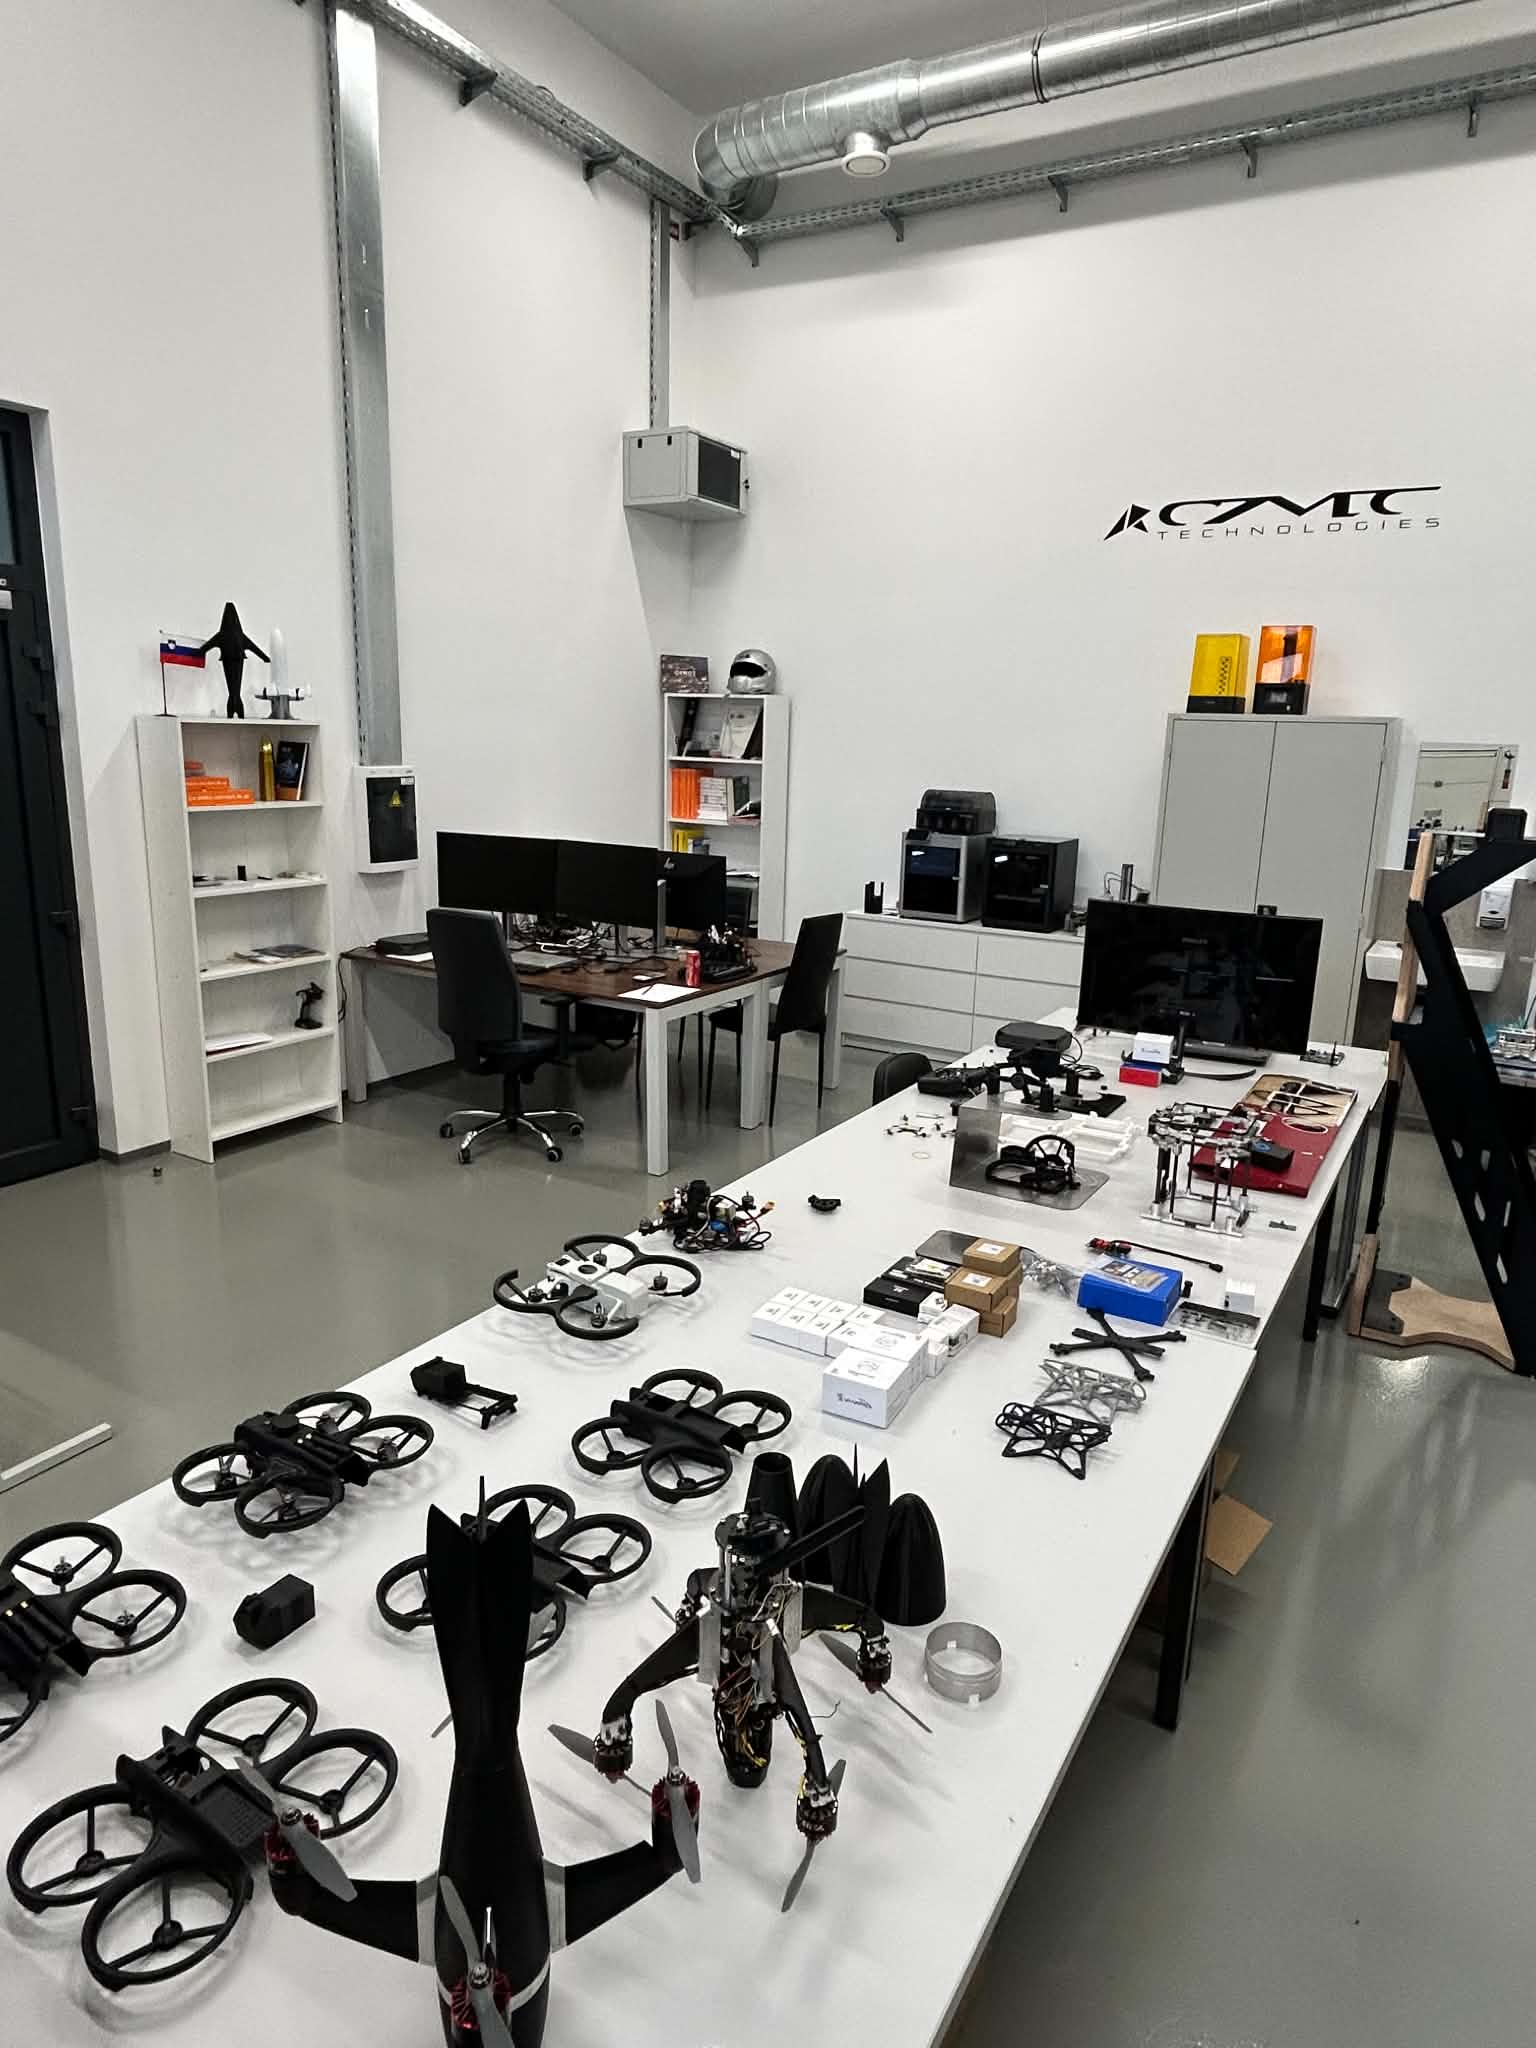
Mechanics, electronics and software come together in one place. We integrate, wire, assemble and test complete systems against documented acceptance criteria — and turn a working prototype into a repeatable production process.
Every Ozmec system is integrated and validated on this line.
ESD-protected assembly · 100% functional test · QMS aligned with EN 9100 (in progress)
- Units functionally tested
- 100%
- Dedicated test rigs & fixtures
- 15+
- Quality gates per build
- 6
- Ozmec platforms integrated here
- 4
Where the disciplines become one system.
Mechanical fit, harness routing and electronic interfaces are checked together — by the engineers who designed them. Integration problems surface on our bench, not in your field trial.
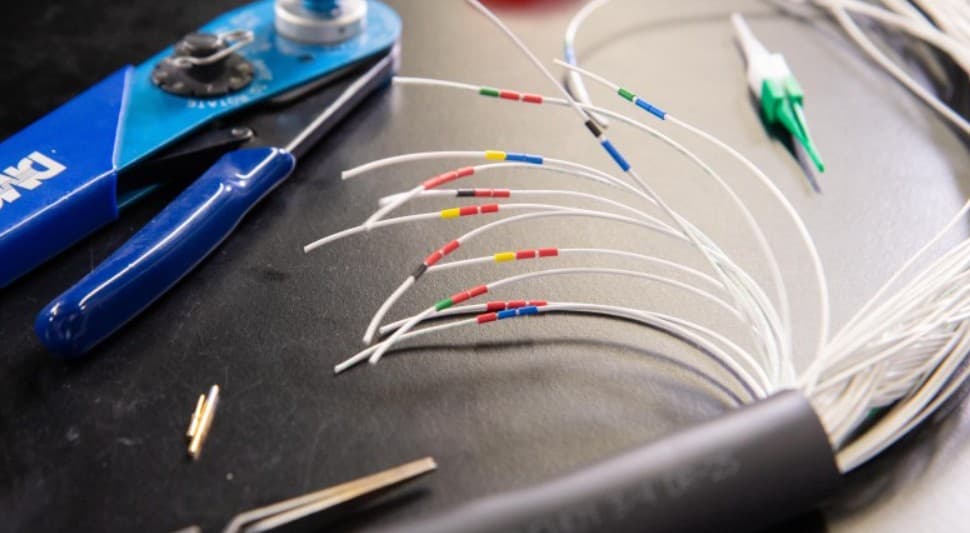
Wiring & harnesses
- Harnesses built to IPC/WHMA-A-620 Class X
- Crimp pull-testing and continuity testing on every harness
- Labelled, documented, routed for vibration
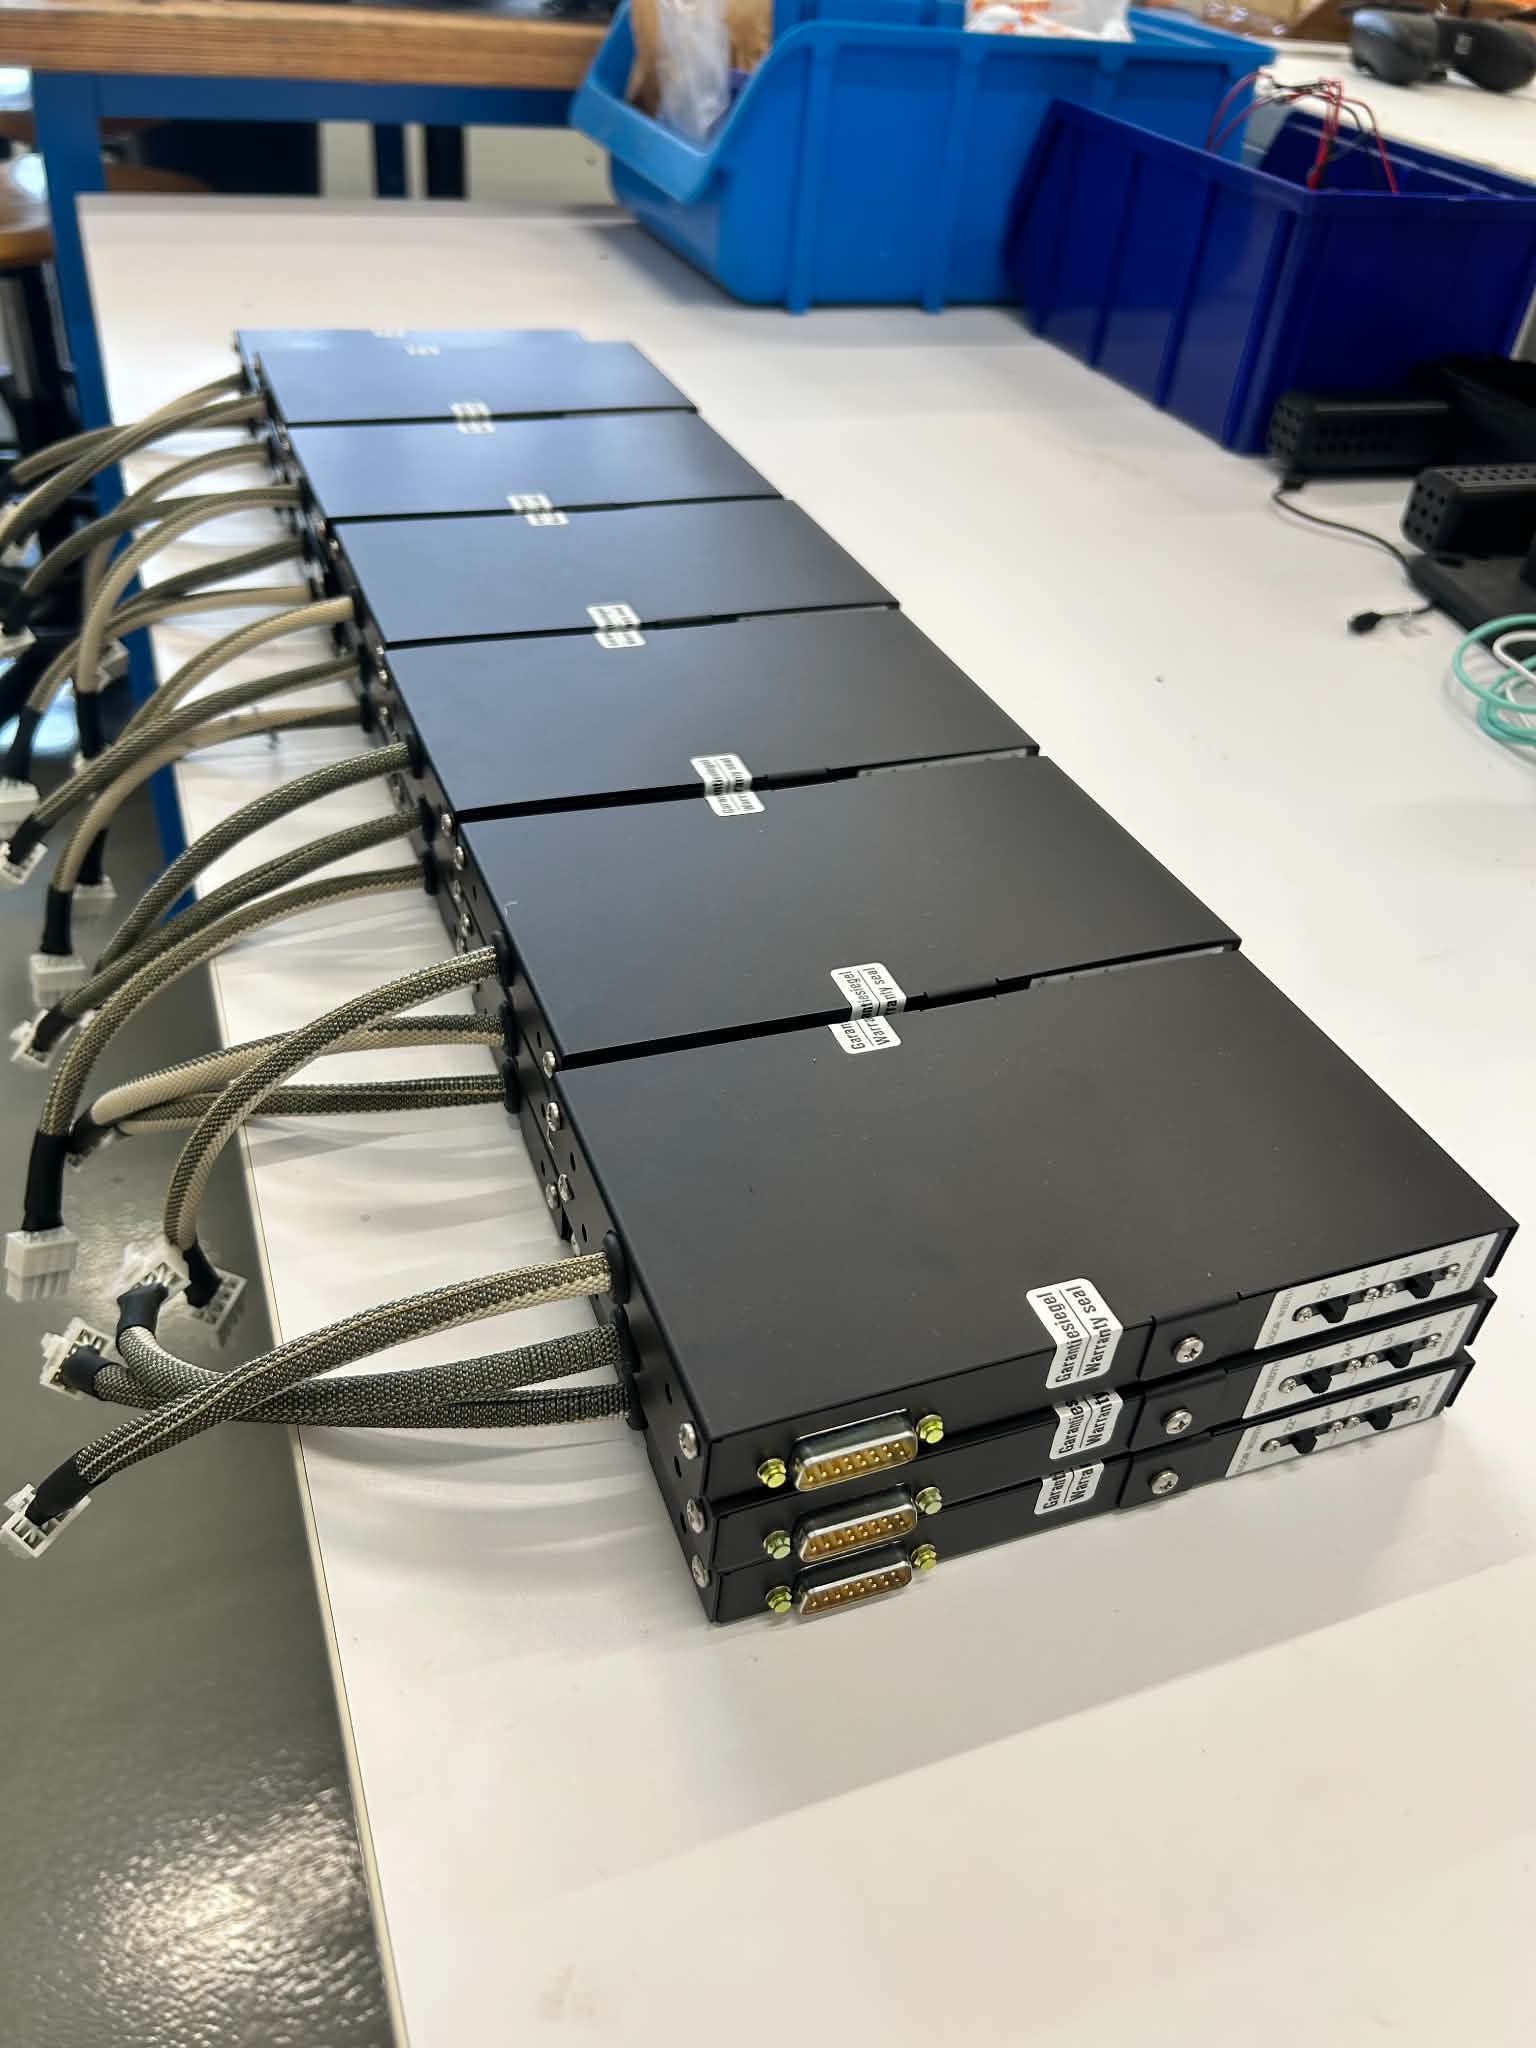
System assembly
- ESD-protected area to EN 61340-5-1
- Torque-controlled fastening, documented per step
- Work instructions with photos for every build
Proof that it works. On paper and in the field.
From the first power-up to field trials, every test runs against written acceptance criteria and ends in a signed report.
Functional testing
Power-up, interfaces, sensors and actuators exercised on dedicated fixtures.
Burn-in
X-hour powered run to catch early-life failures before delivery.
Environmental
Vibration, thermal cycling, IP ingress — to MIL-STD-810 / DO-160 methods.
EMC pre-compliance
Emission and immunity scans before formal certification testing.
Field testing
Validated in real conditions — in the air, on track or on site — with full logging and analysis.
Factory acceptance (FAT)
Acceptance test procedure run with your team — on site or remotely witnessed.
Six quality gates. Built into every build.
Quality is not a final inspection. It runs from incoming parts to release — the same discipline we are preparing to certify under EN 9100.
- Gate 01
Incoming inspection
Parts, PCBs and harnesses verified against drawing and spec.
- Gate 02
In-process control
Checkpoints during integration catch deviations early.
- Gate 03
Functional test
Powered and exercised on fixtures before leaving the bench.
- Gate 04
Final acceptance
Checked against acceptance criteria, released with a signed result.
- Gate 05
Traceability
Serials, batches and records trace every build to its parts.
- Gate 06
Calibrated equipment
Calibrated instruments keep results comparable over time.
From one working unit to a repeatable process.
A demo that works once is not a product. We build the fixtures, procedures and test software that make every unit identical — and hand them over if you produce elsewhere.
- Test rigs
- Custom fixtures and test benches designed and built in-house
- Test software
- Automated test sequences with pass / fail logging per serial number
- Work instructions
- Step-by-step assembly and test procedures, versioned with the design
- Non-conformance
- Deviations recorded, root-caused and closed with corrective actions
- Transfer
- Full process package for production at your site or a partner of your choice
From parts on the bench to accepted system in five steps.
Bring us a design we built, a design you built, or a kit of parts. Every step ends with a documented result.
- 01
Build plan
Assembly sequence, test plan and acceptance criteria agreed with you.
- 02
Pilot build
First units assembled, work instructions written from the real build.
- 03
Validation campaign
Functional, environmental and field tests against the plan.
- 04
Acceptance
FAT with your team, signed acceptance report.
- 05
Series or transfer
Small-series production with us, or full process handover.
What you receive.
Systems you can deploy — and the evidence your quality and procurement teams need to accept them.
- Assembled systems
- Integrated, tested and serialised units ready to deploy
- Test procedures & reports
- ATP, test results per serial number, environmental test reports
- Acceptance documentation
- Signed FAT report and certificate of conformity
- Traceability records
- As-built configuration: parts, batches, firmware versions per unit
- Work instructions
- Versioned assembly and test procedures
- Production-ready process
- Test rigs, test software and documentation for series production
Before you ask.
Can you assemble systems we designed?
Yes. We integrate and test customer designs, including customer-supplied parts, after a short build-readiness review.
Which tests do you run in-house?
Functional, burn-in and field tests in-house; environmental and EMC testing with accredited partner labs. We plan and manage the whole campaign.
Can our team witness acceptance tests?
Yes. Factory acceptance tests can be witnessed on site in Ormož or remotely.
Can you transfer production to our facility?
Yes. We hand over work instructions, test rigs and test software, and support the first builds at your site.
Are you EN 9100 certified?
Not yet. Our quality system is aligned with EN 9100 and certification is in progress, target quarter / year.
Bring us your system. We'll prove it works.
Share your design, quantities and acceptance requirements. Our quality lead replies within 2 working days with a build and test proposal — under NDA if you need it.